 EN

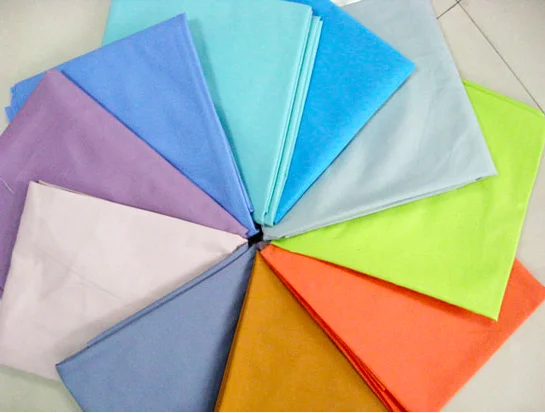
Navigating Hygiene and Performance in Uniform Textiles
Working closely with international healthcare providers, hospitality groups, and industrial manufacturing facilities for over a decade often reveals how quickly a high-performance uniform program can suffer due to microbial accumulation, unpleasant odors, and hygiene concerns. Sourcing uniform textiles in today's fast-moving global marketplace is rarely a simple transaction. As facility managers and corporate buyers increasingly demand enhanced fabric durability, moisture management, and active microbial suppression, the risks associated with untreated or poorly engineered fabrics multiply exponentially. Partnering with a technically advanced supplier of poly cotton uniform fabric transforms a volatile, high-risk supply chain into a formidable competitive advantage, safeguarding wearer health from initial fiber selection all the way through to large-scale commercial laundering. Early technical collaboration also prevents critical hygiene failures that frequently derail workplace compliance schedules and inflate operational replacement budgets unexpectedly, giving procurement teams the absolute confidence needed to succeed in demanding international markets and fast-evolving institutional environments.
The Science of Integrating Antimicrobial Properties into Blended Textiles
A seasoned textile production partner brings far more intrinsic value to the development table than basic weaving capacities or generic catalog options; they offer deep, practical expertise in polymer science, silver-ion infusion, and advanced non-leaching antimicrobial treatments. According to international textile engineering research published by the Textile Institute, a significant percentage of bacterial growth in professional workwear stems directly from moisture retention within cotton-synthetic interfaces. Experienced manufacturers leverage state-of-the-art chemical bonding agents, permanent nano-silver embedding, and advanced finishing lines to ensure that poly cotton uniform fabric performs exceptionally well under rigorous wear and continuous industrial laundering. This high level of technical rigor eliminates costly, time-consuming sample iterations and drastically accelerates overall time-to-market while giving engineering teams absolute peace of mind during large-scale garment manufacturing and seasonal commercial rollouts across diverse global regions and climatic environments.
Balancing Durability, Comfort, and Health Standards
In today's fast-paced global manufacturing landscape, which is frequently marked by stringent workplace health regulations and high hygiene expectations, balancing breathability with microbial protection serves as the absolute core pillar of brand trust and garment continuity. Elite textile manufacturers maintain strategic, long-standing, collaborative relationships with chemical innovators, securing reliable priority allocation for safe, EPA-compliant, and dermatologically tested antimicrobial agents. Furthermore, advanced ISO-certified production facilities implement strict, multi-layered quality control protocols at every single production stage, ranging from meticulous yarn inspection to quantitative antibacterial efficacy testing against staphylococcus and E. coli prior to shipping. This total transparency and strict process consistency ensure that batch-to-batch variation is minimized to near zero, protecting global brands from premature fabric degradation and preserving hard-earned corporate reputations across international retail markets where workplace safety is paramount. Comprehensive testing environments further validate tensile strength, pilling resistance, and anti-odor performance under extreme climatic conditions.
Optimizing Total Cost of Ownership Through Smart Manufacturing
While lower-tier, unverified suppliers may occasionally tempt procurement departments with deceptively low initial unit prices, hidden long-term operational costs—such as rapid odor retention, frequent garment replacement cycles, expensive chemical wash failures, and severely compromised hygiene ratings—frequently decimate corporate budgets. Collaborating with an established provider of poly cotton uniform fabric actively helps optimize comprehensive Total Cost of Ownership. By providing highly durable blended structures, wash-resistant antimicrobial treatments, and robust industrial-grade textiles, professional partners substantially reduce ongoing laundry claims and long-term uniform overhead. Ultimately, investing upfront in superior manufacturing excellence translates directly into unmatched product durability, significantly higher wearer satisfaction, and maximized long-term corporate profitability, ensuring brands stand out for exceptional textile quality and dependable hygiene performance under intense daily pressure. Effective cost optimization also involves minimizing fabric wastage and maximizing resource efficiency across every operational cycle.
Fostering Industry Safety and Workplace Compliance Through Strategic Collaboration
Beyond technical specifications and cost efficiency, choosing the right manufacturing ally establishes a foundation for continuous innovation and rapid market scalability. In a competitive economy where workplace safety standards and hygiene regulations shift year after year, organizations cannot afford to waste valuable operational bandwidth troubleshooting recurring odor issues or struggling with inflexible suppliers. A truly world-class textile partner acts as an extension of internal design and procurement departments, offering proactive engineering feedback, custom finishing modifications, and scalable volume production that adapts seamlessly to shifting market demand. This proactive synergy empowers uniform distributors and corporate buyers to focus fully on core operational growth while leaving textile innovation and quality execution in the hands of trusted specialists.
Empowering Brand Growth and Scaling Success with Hebei Gaibo
Successfully navigating the ongoing complexities of modern textile sourcing requires a reliable, world-class ally who deeply understands both precision fabric engineering and dynamic global commercial logistics. Hebei Gaibo stands out globally as a premier provider of poly cotton uniform fabric, seamlessly combining decades of specialized custom manufacturing expertise with a highly resilient, customer-centric supply chain network. Whether corporate clients require tailored antimicrobial fabric solutions, high-volume uniform rollouts, or specialized technical finishes, Hebei Gaibo consistently delivers uncompromised quality and seamless project execution. Partnering with Hebei Gaibo elevates textile product performance, mitigates manufacturing risks, and secures a lasting competitive edge in the crowded global marketplace, backed by a trusted industry leader dedicated to long-term commercial triumph, consistent quality assurance, and continuous customer satisfaction.
Table of Contents
- Navigating Hygiene and Performance in Uniform Textiles
- The Science of Integrating Antimicrobial Properties into Blended Textiles
- Balancing Durability, Comfort, and Health Standards
- Optimizing Total Cost of Ownership Through Smart Manufacturing
- Fostering Industry Safety and Workplace Compliance Through Strategic Collaboration
- Empowering Brand Growth and Scaling Success with Hebei Gaibo
